Modern packaging and material handling operations depend on conveyor equipment that can move products efficiently while maintaining reliable production flow. Two solutions commonly used in high-speed manufacturing and packaging environments are Table Top Conveyor Systems and Air Conveyor Systems.
The following FAQs explain how these conveyor technologies work, where they are commonly used, and what manufacturers should consider when selecting an engineered conveyor solution.
What are Table Top Conveyor Systems?
Table Top Conveyor Systems use a continuous tabletop-style chain or belt to transport products between processing, packaging, inspection, accumulation, and palletizing operations. They are particularly useful when products require stable support and controlled movement.
Depending on the application, table top conveyors can handle bottles, cans, cartons, containers, cases, packaged products, and other materials.
What are the advantages of Table Top Conveyor Systems?
Table Top Conveyor Systems can provide several operational advantages, including reliable product handling, flexible layouts, controlled product movement, integration with packaging equipment, and the ability to accommodate curves, transfers, merges, and accumulation requirements.
When designed as part of an engineered system, table top conveyors can also help manufacturers improve overall production flow rather than simply move products from one location to another.
What industries use Table Top Conveyor Systems?
Table top conveyors are commonly found in food and beverage, consumer packaged goods, pharmaceutical, personal care, container manufacturing, and general packaging operations.
The correct conveyor configuration depends on factors such as product dimensions, production rate, container stability, sanitation requirements, available floor space, and upstream and downstream equipment.
What are Air Conveyor Systems?
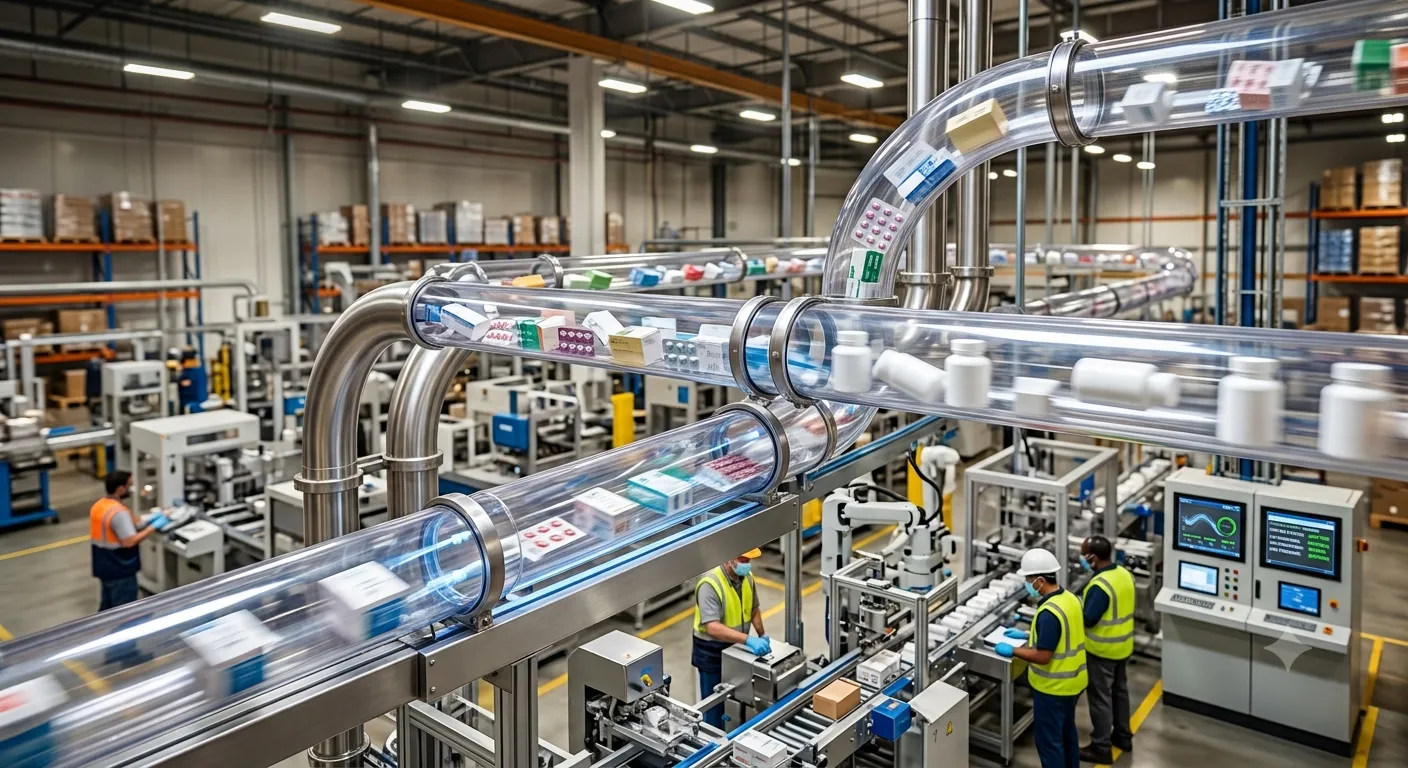
Air Conveyors Systems use controlled airflow to transport lightweight containers or products through a production environment. They are frequently used for high-speed handling of empty PET bottles and similar lightweight containers.
Instead of relying exclusively on a conventional conveyor surface, air conveyor technology uses strategically directed air to move containers efficiently through the system.
When should a manufacturer consider an Air Conveyor System?
An Air Conveyor System may be appropriate when an operation needs to transport lightweight containers at high production speeds, particularly between container manufacturing, filling, and packaging processes.
The system should be engineered around container geometry, line speed, routing, environmental conditions, and the requirements of connected equipment.
Can Table Top Conveyor Systems and Air Conveyor Systems be integrated?
Yes. In many production environments, different conveyor technologies are used together as part of a larger material handling solution.
For example, an Air Conveyor System may transport lightweight empty containers toward filling equipment, while a Table Top Conveyor System handles filled or packaged products farther downstream.
The key is designing the complete system around the production process rather than treating each conveyor as an isolated piece of equipment.
Can conveyor systems include accumulation?
Yes. Accumulation can provide an important buffer between production processes. Properly engineered accumulation allows sections of a line to continue operating during brief downstream interruptions and can reduce unnecessary stops.
The appropriate accumulation strategy depends on the product, required capacity, line speed, available space, and operational objectives.
Why choose an engineered conveyor system?
A conveyor system should do more than connect Point A to Point B. An engineered system considers how products enter, travel through, accumulate within, and exit the conveyor network.
By evaluating speeds, transfers, controls, accumulation, equipment interfaces, and facility constraints together, manufacturers can develop a conveyor solution designed around the needs of the complete production line.